Tighter Isn't Always Better: Understanding How Tolerance Decisions Shape Fabrication Cost and Schedule
There is a persistent assumption in engineering culture that tighter tolerances are inherently superior—that specifying ±0.001" instead of ±0.010" signals rigor, professionalism, and a commitment to quality. In some applications, that assumption is correct. In many others, it quietly drives up project costs, extends lead times, and introduces production complexity that serves no functional purpose.
Understanding the true relationship between tolerance specifications and project economics is not a matter of cutting corners. It is a matter of engineering discipline—and it begins long before the first piece of metal is cut.
What Tolerances Actually Control
A tolerance specification defines the permissible variation from a nominal dimension. When a drawing calls for a hole diameter of 0.500" ±0.005", the fabricator is permitted to produce any result between 0.495" and 0.505" and still deliver a conforming part. Tighten that band to ±0.001", and the acceptable window narrows to just 0.002"—a range that demands fundamentally different equipment, tooling, and verification methods.
This is where many project conversations go wrong. Engineers often apply tight tolerances across an entire drawing without distinguishing between features that are functionally critical and those that simply need to be "close enough." The result is a uniform specification burden that forces fabricators to treat every dimension as if it were a precision bearing seat—regardless of whether it ever contacts another component.
How Tolerance Requirements Travel Through Production
The impact of a tolerance specification is rarely confined to a single operation. It propagates through the entire production sequence in ways that are not always visible on a cost estimate.
Tool and machine selection is the first point of friction. Standard press brakes, plasma cutters, and MIG welding setups are optimized for efficiency within moderate tolerance ranges. When specifications tighten significantly, shops must route work to more precise equipment—CNC machining centers, precision grinding stations, or laser systems with tighter beam control. These machines carry higher operating costs and, critically, higher demand from other jobs in the queue.
Fixturing and setup complexity increases in parallel. Holding a part to within a few thousandths of an inch across multiple operations requires purpose-built fixtures, careful datum selection, and extended setup times. A job that would take thirty minutes to set up under standard tolerances may require two hours or more when precision is non-negotiable.
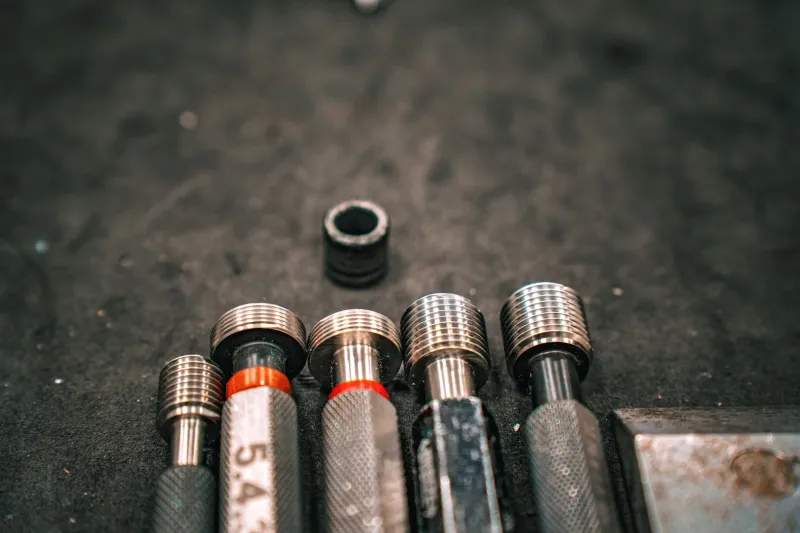
Inspection and verification represent perhaps the least-discussed cost driver. Standard dimensional checks using calipers and tape measures are fast and inexpensive. Tight tolerances often require coordinate measuring machine (CMM) inspection, optical comparators, or laser measurement systems—each of which adds time, labor, and equipment utilization cost to every part that passes through quality control. When first-pass yield drops because the specification window is narrow, inspection time compounds further.
Scheduling displacement is the cumulative result. Jobs requiring precision equipment compete for limited machine time. A single tight-tolerance component introduced into a production schedule can push other work, creating ripple effects that extend lead times across an entire order.
The Economics Are Nonlinear
One of the most important things decision-makers can internalize is that tolerance tightening does not produce linear cost increases. Moving from a ±0.010" tolerance to ±0.005" might add modest cost. Moving from ±0.005" to ±0.001" may multiply that cost several times over. The relationship between dimensional precision and production expense follows a curve that steepens sharply as specifications approach the limits of standard manufacturing capability.
This nonlinearity exists because tight tolerances often cross thresholds that require categorically different production approaches—not just incremental adjustments. The difference between a part that can be produced on a standard CNC lathe and one that requires precision grinding is not a matter of degree. It is a difference in process, equipment class, and operational overhead.
A Framework for Tolerance Decision-Making
Engineering teams that engage fabricators early in the design process gain access to a practical filter for tolerance decisions. The core question is straightforward: What does this dimension actually control?
For each toleranced feature, consider:
- Functional criticality: Does this dimension directly affect fit, function, or safety? If a shaft must mate with a bearing, the tolerance is non-negotiable. If a bracket mounting hole simply needs to align with a bolt pattern, a standard tolerance is almost always sufficient.
- Assembly interface: Does this feature contact or interact with another component? Features that interface with mating parts warrant tighter control. Features that exist in open space typically do not.
- Inspection practicality: Can the tolerance be verified with standard shop tooling, or does it require specialized measurement equipment? If the latter, factor that cost explicitly into the project budget.
- Downstream serviceability: Will this part be replaced in the field? If so, tighter tolerances that create interchangeability may justify their cost. If the part is a one-time installation, that justification weakens.
Applying this filter systematically—feature by feature, rather than applying a blanket specification across an entire drawing—can meaningfully reduce production complexity without compromising the performance characteristics that actually matter.
When Tight Tolerances Are Worth Every Penny
None of this is an argument against precision. There are applications where tight tolerances are not only justified but essential. Pressure vessel components, structural connections subject to dynamic loading, precision motion systems, and safety-critical assemblies all demand dimensional control that cannot be relaxed without consequence.
In these contexts, the cost of tight tolerances is not a penalty—it is the price of performance. The goal is not to avoid precision but to apply it deliberately, in the places where it earns its keep.
The fabricators best positioned to help customers make these distinctions are those with deep application experience across multiple industries. A shop that has produced components for aerospace, heavy industry, and commercial construction simultaneously understands both what precision demands and what standard practice can reasonably achieve.
The Collaborative Advantage
The most effective tolerance conversations happen before a drawing is finalized. When engineering teams bring fabricators into the design review process early, they gain a ground-level perspective on which specifications create disproportionate production burden and which are essential to part performance.
This is not a request for fabricators to override engineering judgment. It is an invitation to apply manufacturing knowledge in service of better engineering outcomes. A fabricator who flags that three features on a drawing are specified to tolerances tighter than the assembly actually requires—and who can demonstrate why—is delivering value that no cost estimate can fully capture.
At GSS Fabrication, this kind of upstream engagement is a standard part of how we approach complex projects. Our engineering team reviews drawings not just for producibility but for specification efficiency—identifying opportunities to align tolerance requirements with functional need before production begins.
Precision Where It Matters, Efficiency Everywhere Else
The goal of sound tolerance specification is not uniformity. It is discrimination—the ability to distinguish between the dimensions that define a part's performance and those that simply describe its geometry. Applied with that discipline, tolerance decisions become a competitive advantage: parts that perform as designed, produced at cost structures that reflect genuine manufacturing requirements rather than specification conservatism.
Tighter is not always better. Better is better. And better, in fabrication, means specifying exactly as much precision as the application demands—and no more.